Description
Technical Overview
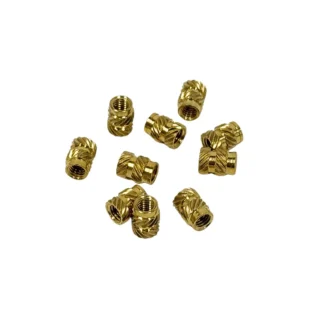
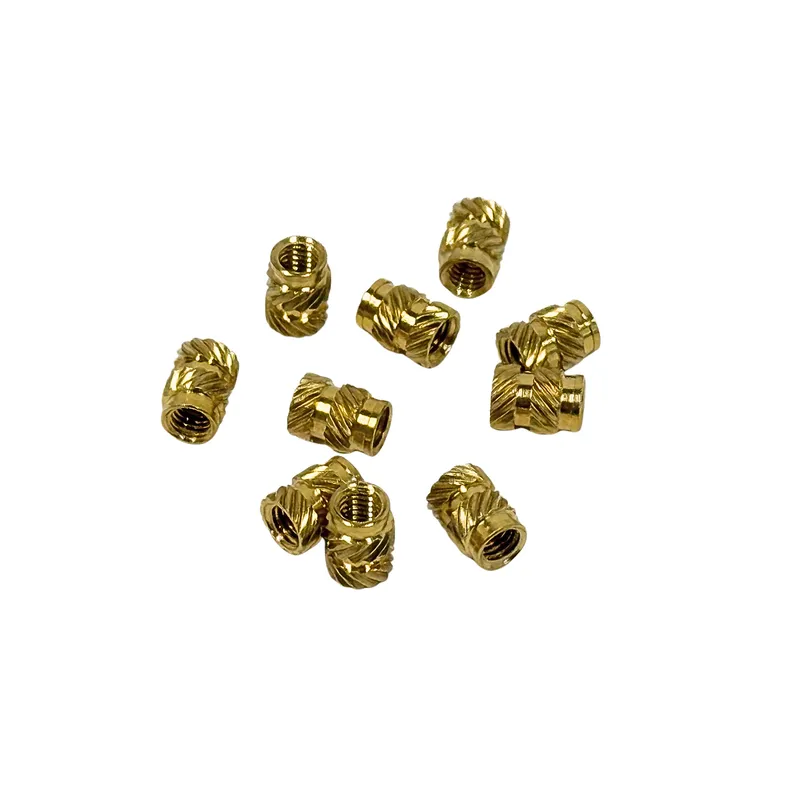
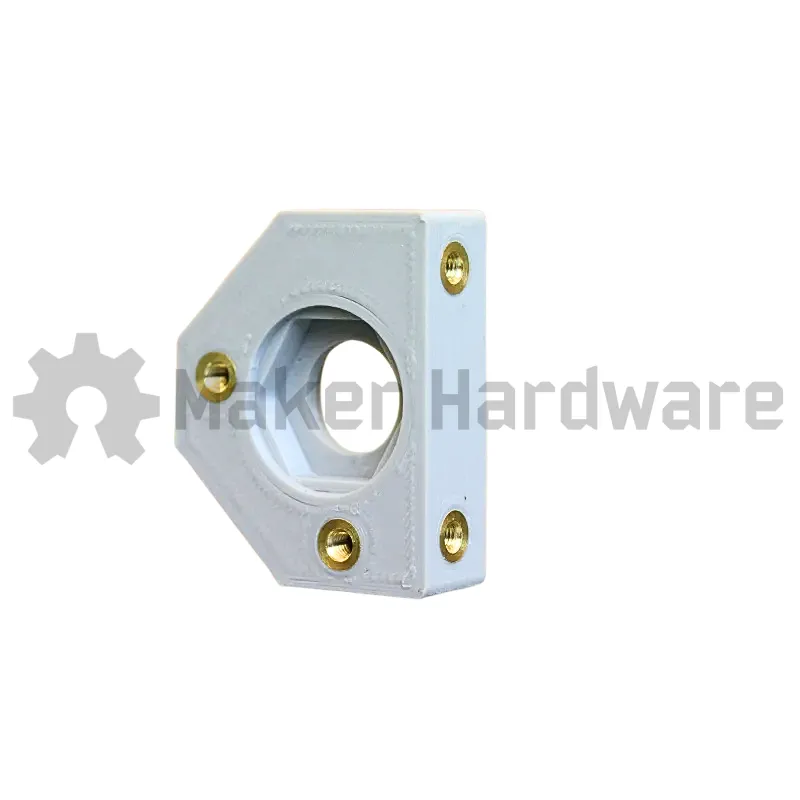
Heat set threaded insert provides durable, reusable metal threads in 3D printed parts and plastic components. To install these components, technicians heat the brass body and press it into a pre-formed hole. This process melts the surrounding material. The plastic then reforms around the insert’s external knurling.
This installation method creates a solid metal thread. The resulting thread resists stripping and wear during repeated assembly and disassembly. Furthermore, these inserts distribute mechanical loads over a wider surface area. Consequently, they provide a more robust fastening solution than driving screws directly into soft materials.
Applications
These inserts provide essential high-strength screw connections for 3D printed enclosures, mechanical assemblies, and structural parts. Manufacturers frequently use them in prototyping and end-use production. In these settings, workers must securely fasten components and occasionally service them without damaging the base material.
In mechanical builds, engineers prefer the heat set threaded insert for joints subject to vibration or tension. These components significantly reduce the risk of thread failure compared to standard self-tapping screws. Finally, they maintain compatibility with a variety of thermoplastics commonly used in FDM and SLA printing processes.
Maker Store Tips and Tricks
-
Use a soldering iron with a specialized heat-set tip to ensure even heat distribution and vertical alignment during installation.
-
Ensure the pre-drilled or printed hole diameter is slightly smaller than the insert’s outer diameter to allow for proper material displacement.
-
Avoid over-heating the insert, as excessive heat can cause the plastic to degrade or ooze into the internal threads.
-
Allow the plastic to fully cool and solidify before attempting to thread a screw into the insert.